L O A D I N G
Proven Expertise

Our Excellence

Catalyst Handling Project
Catalyst Handling

Catalyst Handling Project

Shop Fabrication Project
Shop Fabrication

Industrial Fabrication Project

Mechanical Maintenance

Plant Mechanical Maintenance

Tank Cleaning
Tank Cleaning

Tank Cleaning & Sludge Processing

Chemical Cleaning
Chemical Cleaning

Chemical Decontamination Project

Plant Commissioning
Plant Commissioning

Industrial Plant Commissioning

Manpower Services
Manpower Services

Skilled Industrial Workforce

Rental Services
Rental Services

Industrial Equipment Rental

INDUSTRIAL SERVICES

CASE STUDIES

HOME / CASE STUDIES

Case Studies

Case Studies

Turning Ideas Into Measurable Results

Every project below is a real industrial mandate — the constraint we were handed, the method we executed, and the number the client could verify afterwards. Capability is measured by what changes once the work is finished.

Scroll to explore

The Archive

The Archive

Execution stories

Selected mandates across catalyst handling, mechanical restoration, decontamination and commissioning — each one reduced to the challenge, the method and the number.

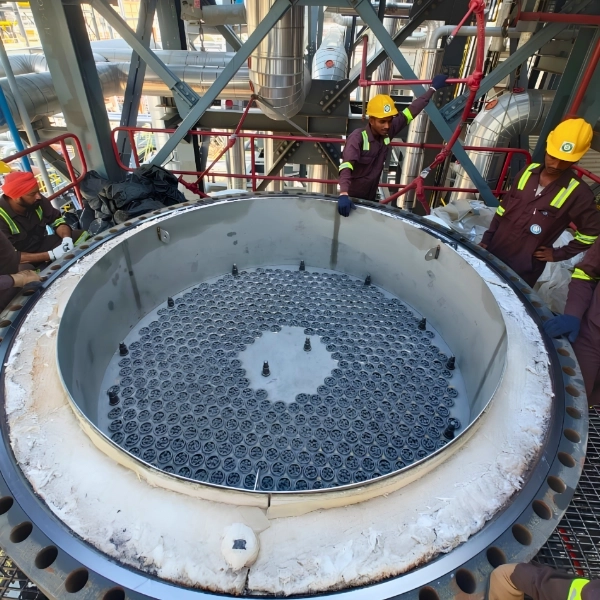
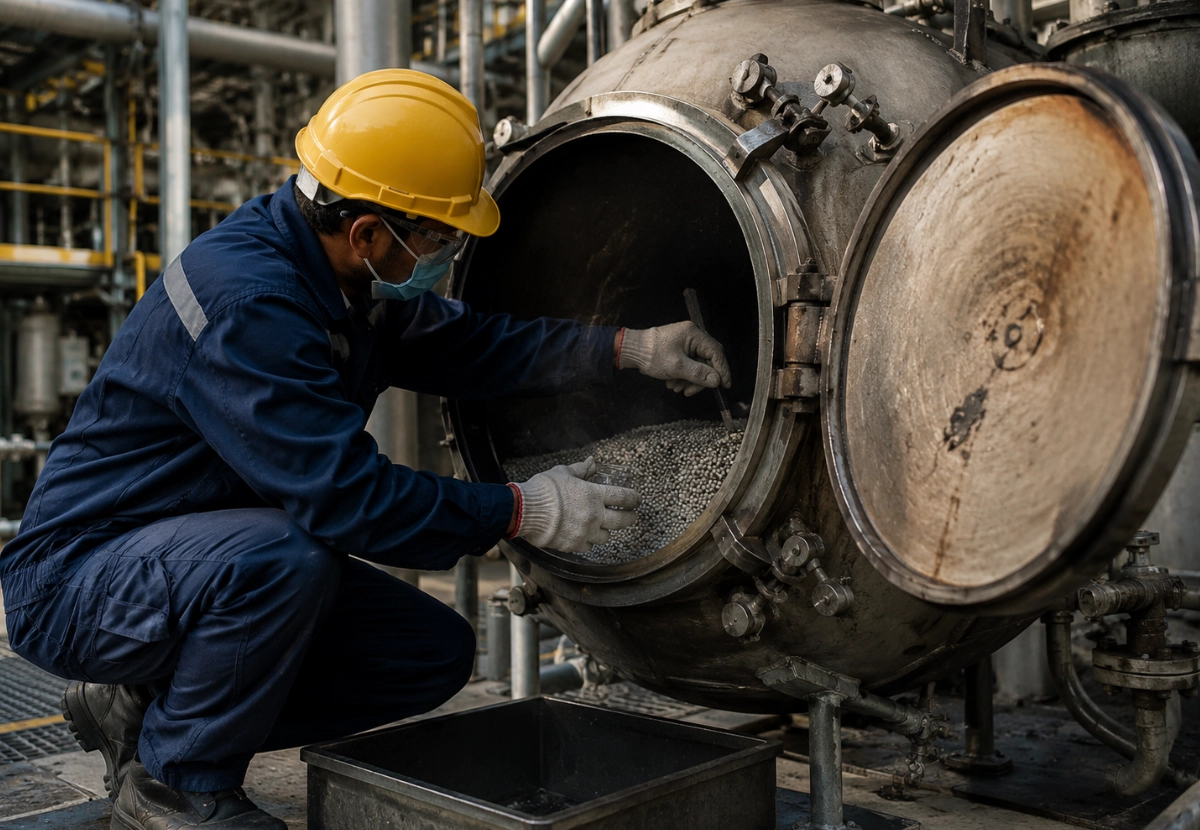
Catalyst extraction from a PSA vessel under nitrogen 01 Catalyst Division
Oil & Gas IDLH Entry ATEX Rated

PSA Vessel Extraction

Catalyst extraction from a PSA vessel under nitrogen 01 Catalyst Division
  • Challenge:A Pressure Swing Adsorption unit required a full catalyst changeout under a strict 100% IDLH nitrogen atmosphere.
  • Solution:ATEX-rated continuous pneumatic vacuum systems with continuous gas monitoring, minimising dust generation and carry-over.
  • Result:An unprecedented 96% yield recovery of the precious metal catalyst, with the vessel returned clean and certified.
96% Noble metal recovery
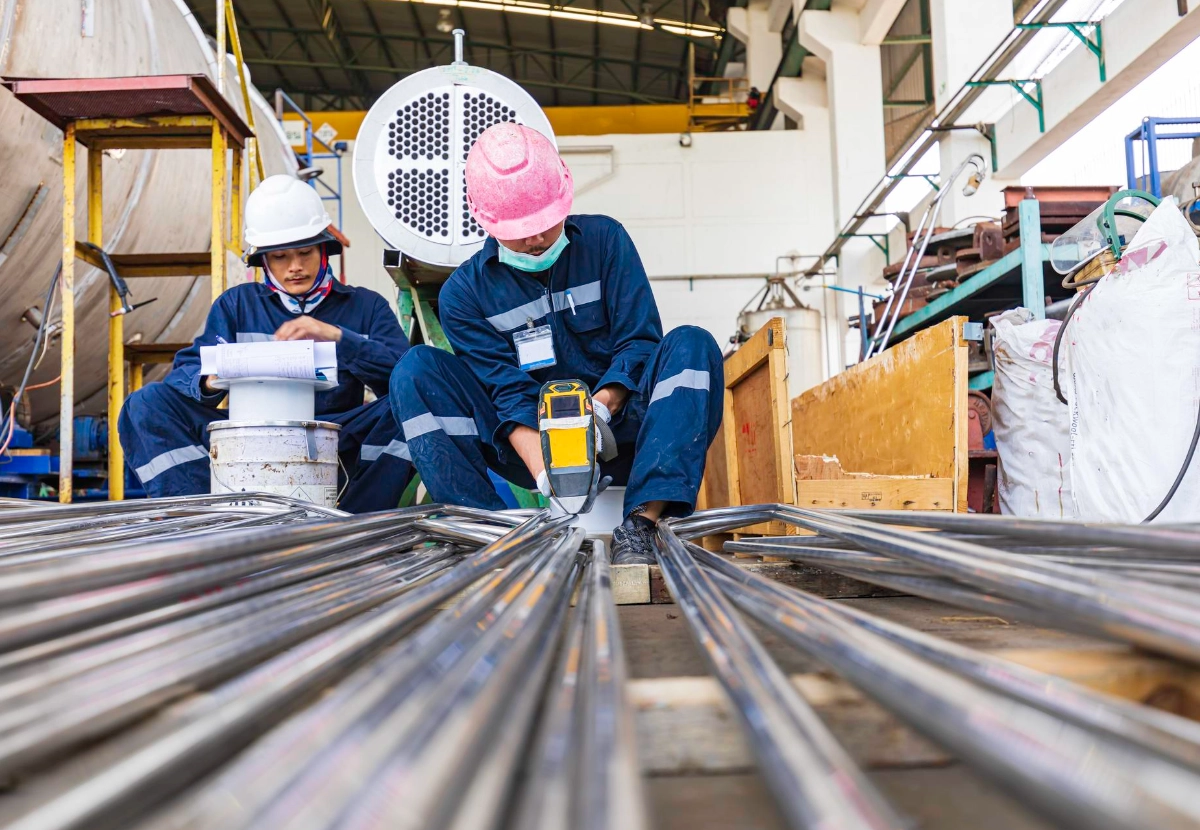
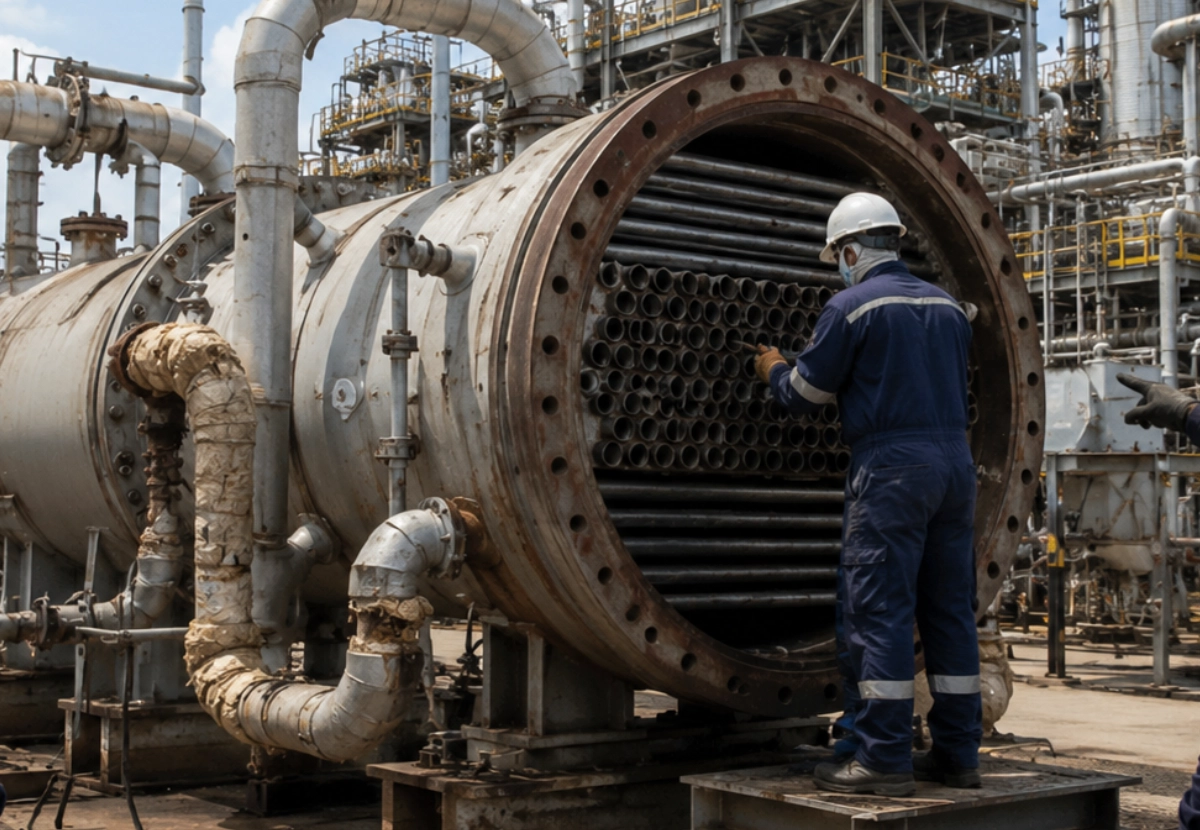
Precision retubing of a crude pre-heat exchanger bundle 02 Mechanical Division
Refining Heat Transfer Hydro-Test

Exchanger Retubing

Precision retubing of a crude pre-heat exchanger bundle 02 Mechanical Division
  • Challenge:Fouling and tube degradation had cost a crude pre-heat train 40% of its thermal efficiency.
  • Solution:Extracted the 20-tonne bundle, removed every tube, then precision-rolled 1,200 new alloy tubes to specification.
  • Result:First-pass hydro-test clearance, with pressure drop restored from 2.8 bar to 0.4 bar.
1,200+ Alloy tubes rolled
Automated hydro-jetting inside a 50,000 MT crude storage tank 03 Environmental Services
Storage Pyrophoric Risk Zero-LEL

Tank Decontamination

Automated hydro-jetting inside a 50,000 MT crude storage tank 03 Environmental Services
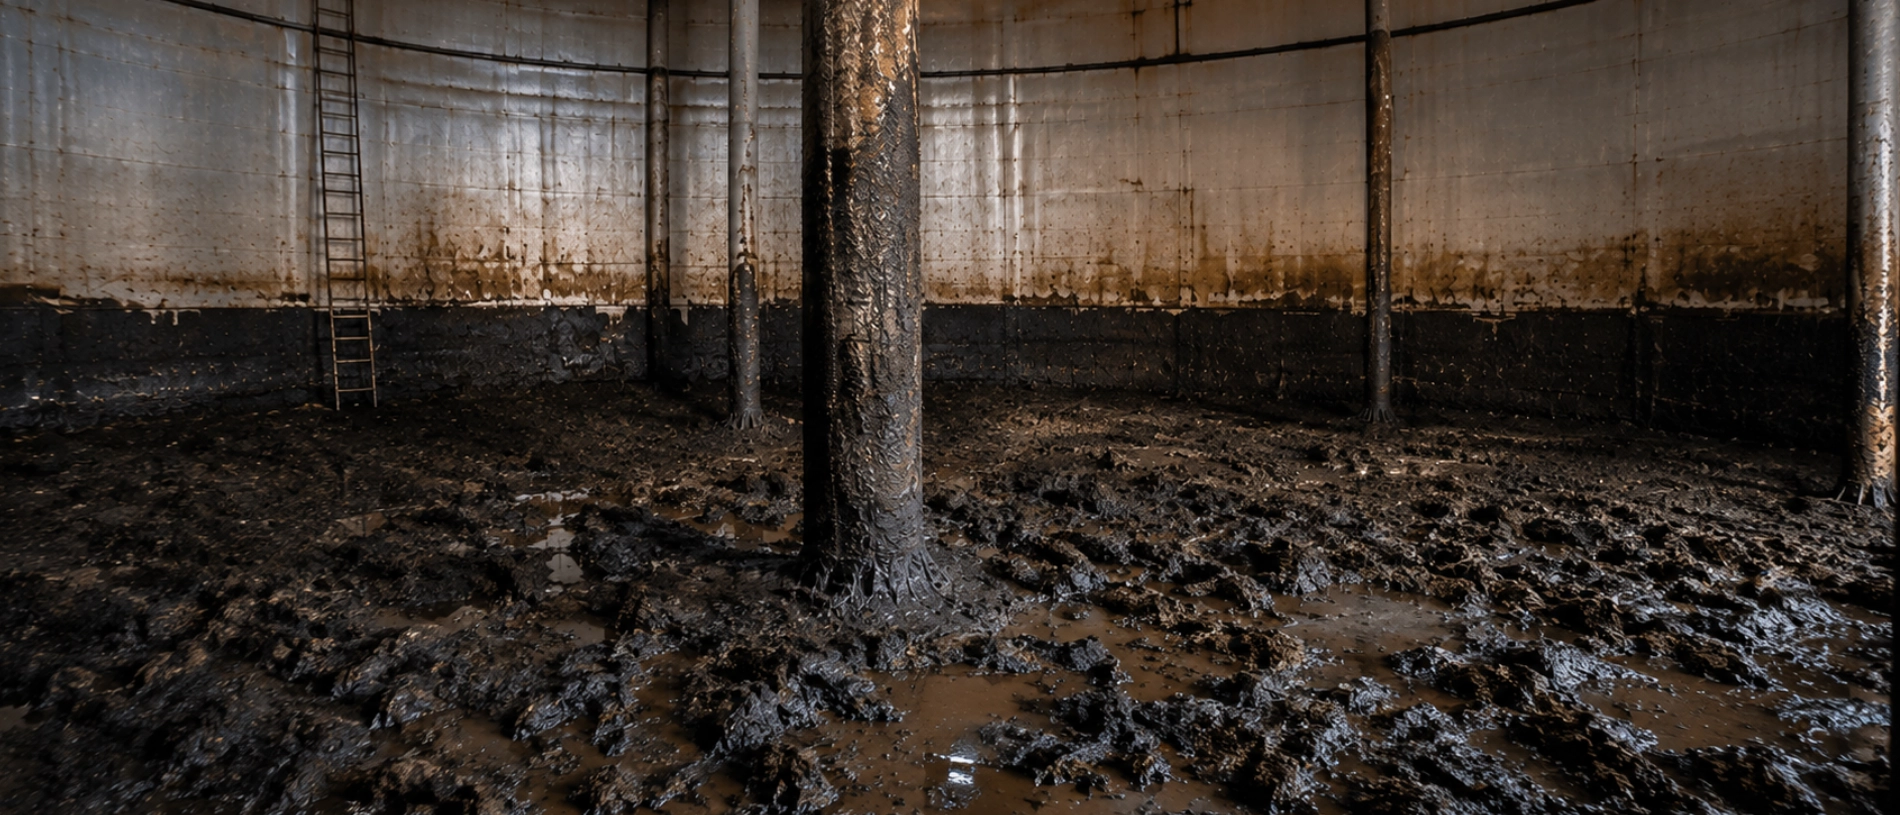
  • Challenge:A 50,000 MT crude storage tank presented heavy sludge compaction and active pyrophoric risk before entry could be authorised.
  • Solution:Automated 3D hydro-jetting paired with chemical oxidisers, run to a controlled sequence with continuous atmospheric monitoring.
  • Result:90% of the hydrocarbon content recovered and returned to process, with the tank certified to a zero-LEL environment.
90% Hydrocarbon recovery
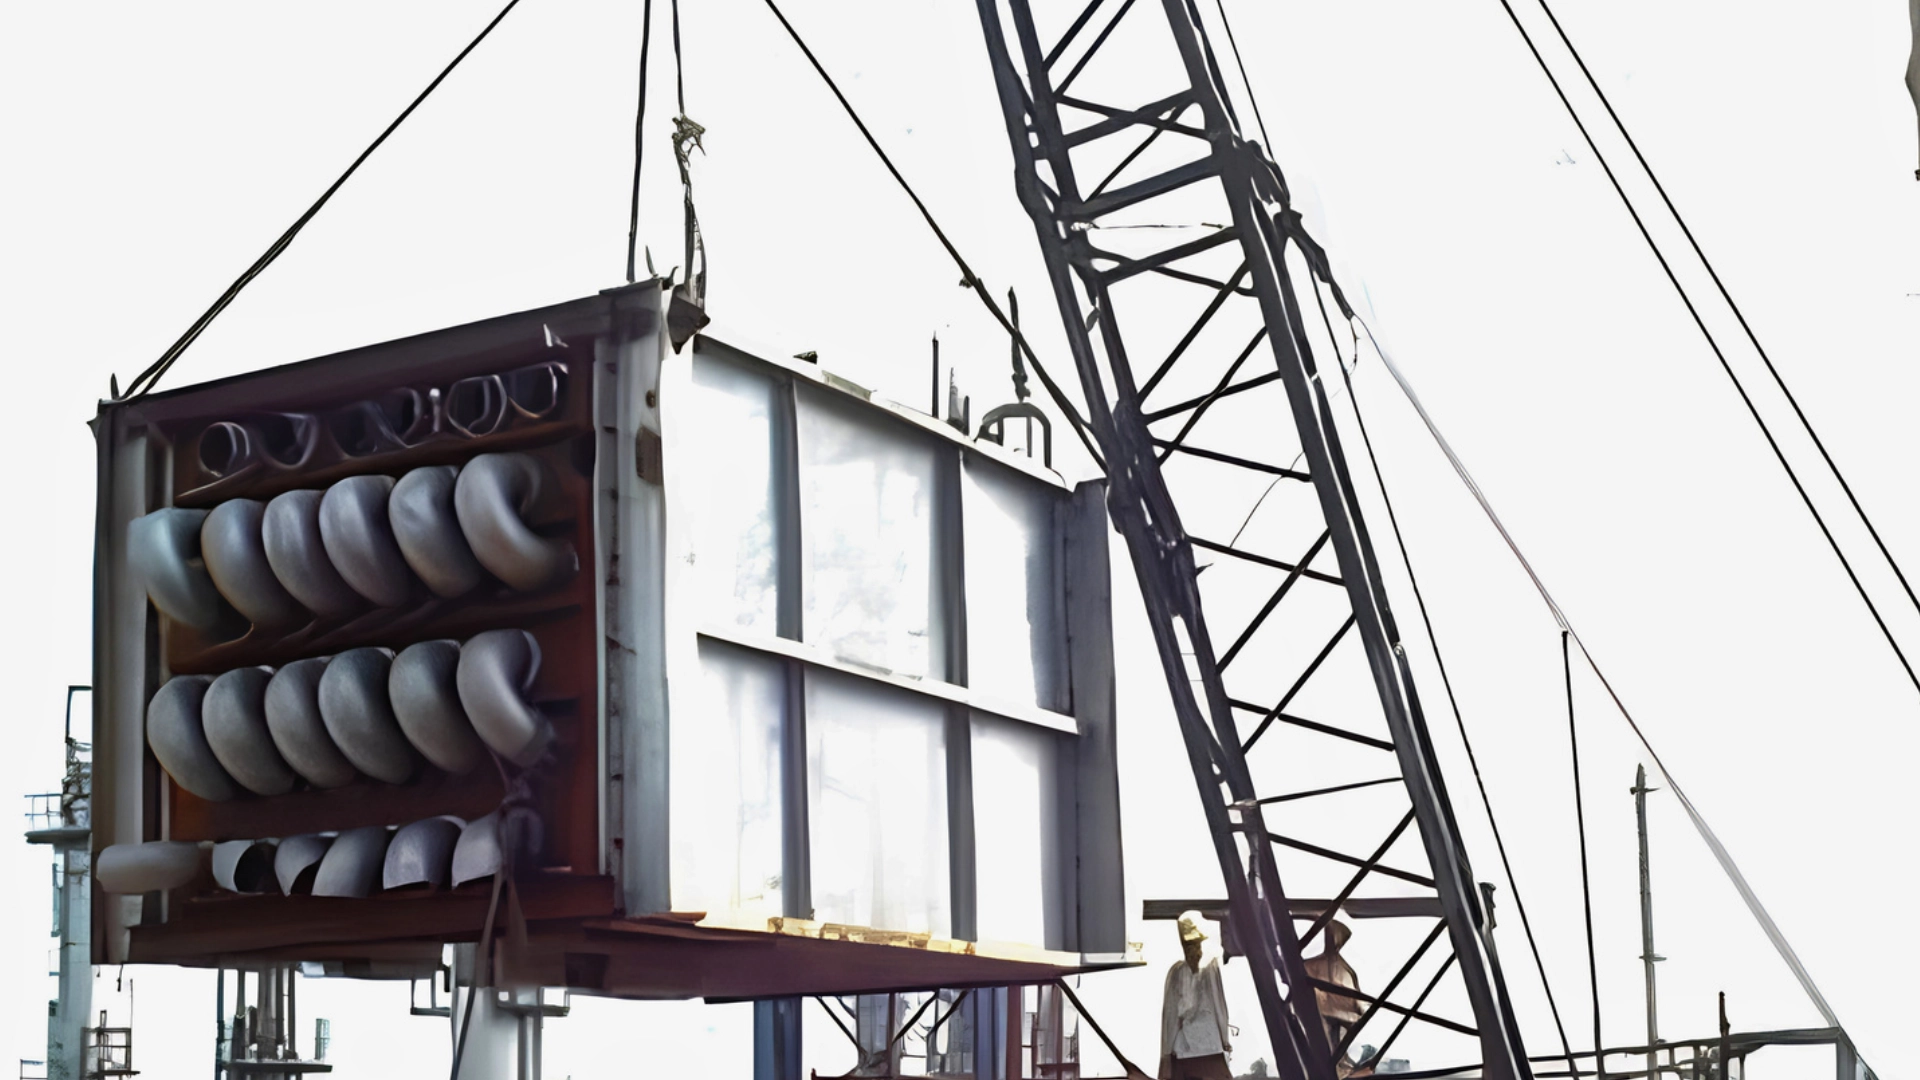
Reformer duct bank installation and alignment 04 Commissioning
Fertiliser Flue Gas Alignment

Reformer Duct Bank Installation

Reformer duct bank installation and alignment 04 Commissioning
  • Challenge:Flue gas duct banks had to be installed to tight alignment tolerances around a live reformer with restricted crane access.
  • Solution:Staged lifts to an engineered rigging plan, with laser alignment verified at every set-down before release.
  • Result:All duct banks set within tolerance at first attempt, with no rework and no impact on the commissioning sequence.
100% First-pass alignment
Fired heater overhaul during a plant shutdown 05 Shutdown Operations
Refining Confined Space 24/7 Shifts

Fired Heater Overhaul

Fired heater overhaul during a plant shutdown 05 Shutdown Operations
  • Challenge:Coil replacement and refractory repair inside a fired heater, scheduled against a fixed restart date with no float.
  • Solution:Round-the-clock shift rotation under a Primavera P6 schedule, with permit control and confined-space rescue cover maintained throughout.
  • Result:Heater returned to service on the planned restart date with all inspection hold points cleared first time.
0 Schedule slippage (days)
Results at a Glance

Measured after handover

Execution is judged by what changes once the crew has demobilised. These are the aggregate numbers across the mandates on this page.

50+ Projects Delivered

Critical-path turnarounds, emergency shutdowns and plant commissioning mandates executed since 1974.

25+ Industries Served
600+ Tradesmen Mobilised
96% Noble Metal Recovery
95% Client Retention
1,200+ Tubes Precision Rolled

Before → After

Before → After

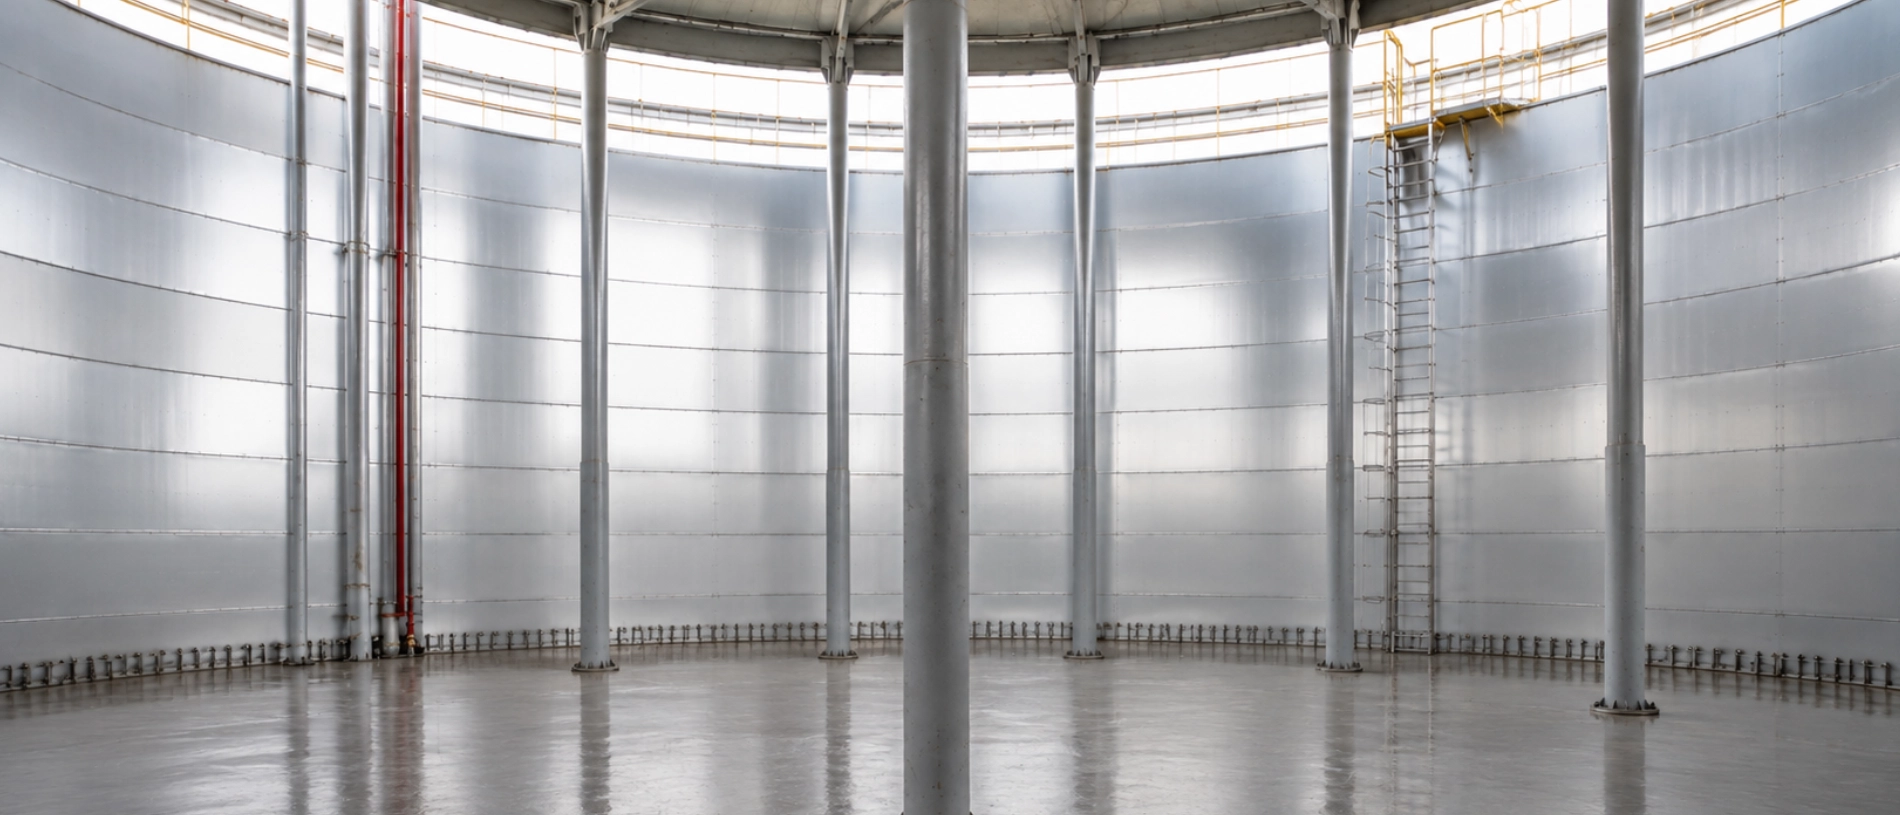
A 50,000 MT tank, transformed

Drag the handle to compare the tank as received against the same tank certified for entry.

Crude storage tank before decontamination, heavy sludge compaction The same tank after decontamination, certified zero-LEL Before After
Before

Compacted and unsafe

Heavy sludge compaction across the floor with active pyrophoric risk. Entry could not be authorised and the tank was out of service indefinitely.

Our Approach

Automated, then verified

Automated 3D hydro-jetting paired with chemical oxidisers, run to a controlled sequence with continuous atmospheric monitoring at every stage.

After

Certified and recovered

Zero-LEL environment certified for entry, with 90% of the hydrocarbon content recovered and returned to process rather than disposed of.

Let’s Deliver Industrial Excellence Together

Partner with us for safe, reliable, and efficient industrial services delivered with quality, expertise, and a commitment to excellence.